Scaling Sustainable Packaging: The Unfiltered Truth About Recyclable Mono-Material Design
Sustainable packaging is no longer a corporate side project—it is an operational imperative. For brand owners, supply chain directors, and packaging engineers, transitioning away from multi-layer laminates toward a single-material approach has become the definitive strategy for real-world circularity. Among the available options, recyclable mono-material packaging stands out as the most scalable, technically viable, and economically sound route to meeting global compliance demands without compromising barrier protection.
Poutan, making the shift is far from plug-and-play. Moving to a unified material structure requires unlearning decades of flexible packaging conventions, navigating strict international regulations, and re-engineering high-speed packaging lines.
Why Legacy Flexible Packaging Fails the Recyclability Test
To appreciate why mono-materials are dominating the sustainable packaging conversation, we first have to look at why classic flexible films fail at the sorting facility.
Pou dè dekad, flexible packaging relied on multi-layer laminates—typically combining PET for print quality and heat resistance, aluminum foil for light and oxygen barriers, ak polyethylene (PE) oswa polypropylène (PP) for sealing strength. While these composite structures offer exceptional shelf life and product protection, they create a mechanical recycling nightmare:
- Separation Complexity: Standard Material Recovery Facilities (MRFs) use optical sorting and sink-float tanks. They cannot cost-effectively delaminate welded, microscopic layers of different polymers.
- Contamination Risk: Processing mixed-plastic laminates results in downcycled, brittle resins with low economic value and poor tensile properties.
- Incineration or Landfill Fate: Consequently, billions of flexible pouches end up in energy-recovery incinerators or landfills every year, despite being technically made of “recyclable resins.”
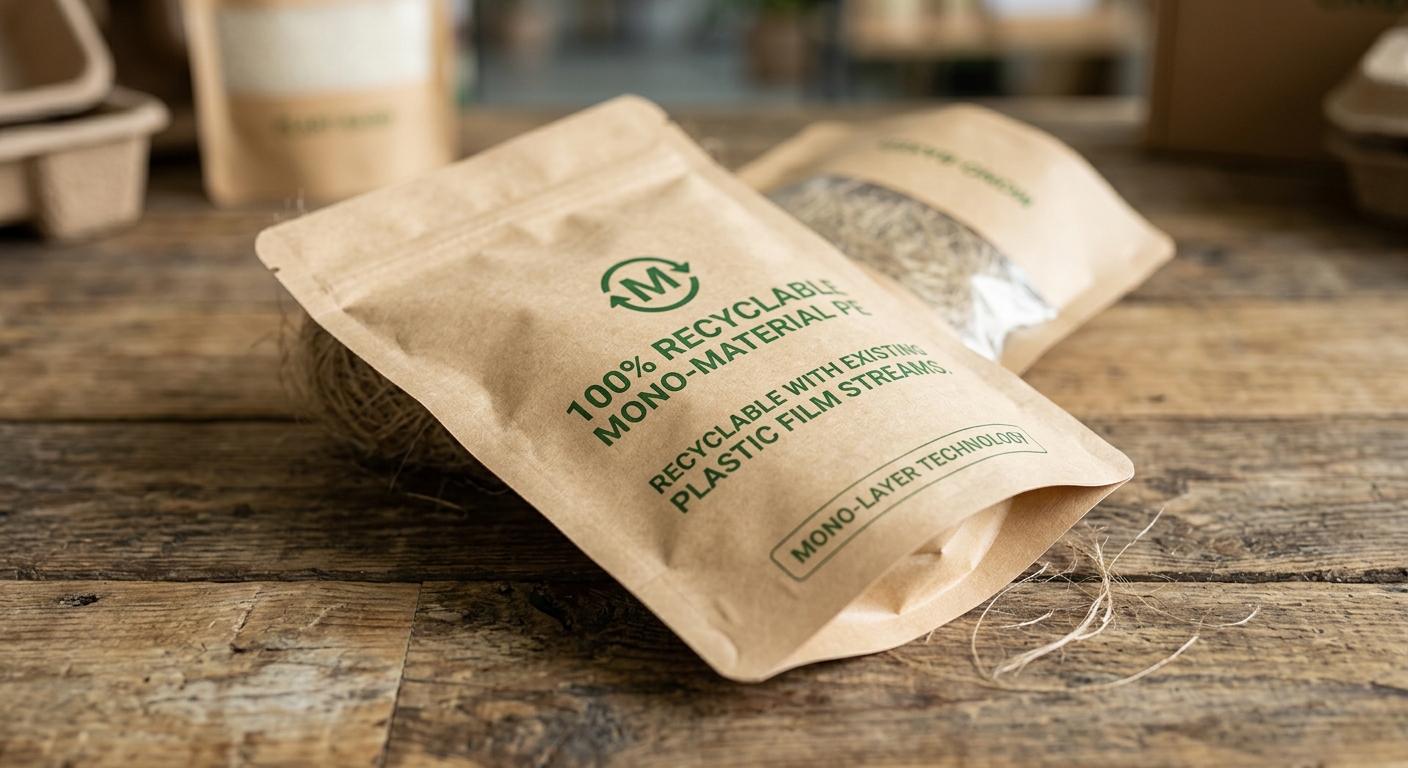
Recyclable mono-material structures solve this fundamental design flaw by engineering the entire package—barrier layers, structural films, and sealant layers—from a single polymer family, tipikman 100% Polyethylene (PE) oswa 100% Polypropylène (PP).
Technical Advances in Mono-Material Engineering
Istorikman, swapping out a multi-layer composite for a single polymer meant sacrificing structural integrity, rezistans chalè, or shelf-life performance. A standard PE pouch, pa egzanp, would warp or melt under traditional heat-sealing jaws, while failing to keep oxygen and moisture out.
Recent material science breakthroughs have largely bridged this gap:
1. Machine Direction Orientation (MDO)
MDO technology stretches PE or PP film in the machine direction during extrusion. This alters the molecular orientation, dramatically improving tensile strength, klète optik, rèd, ak rezistans chalè. MDO-PE films can now replace PET as an outer printing layer, allowing packaging lines to run at competitive line speeds without thermal deformation.
2. High-Performance Barrier Coatings
Achieving low Oxygen Transmission Rates (OTR) and Water Vapor Transmission Rates (WVTR) without aluminum foil used to be impossible. Jodi a, vacuum-deposited Silicon Oxide ($\tèks{SiO}_x$), Aluminum Oxide ($\tèks{AlO}_x$), or ultra-thin EVOH (Ethylene vinyl alkòl) layers are applied to mono-PE or mono-PP substrates. Crucially, as long as non-PE functional layers stay under global threshold limits (typically under 5% of total package weight), the container retains its “100% resikle” classification under standard guidelines like RecyClass and APR (Association of Plastic Recyclers).
3. Broad-Window Sealant Resins
Metallocene-catalyzed resins allow exact tailoring of melting points. By combining a high-density PE outer skin with a low-melting metallocene LLDPE sealant layer, converter plants achieve a wide heat-sealing window—ensuring tight seals at high line speeds without burning through the outer surface.
Regulatory Drivers and Commercial Urgency
The migration toward recyclable mono-material designs isn’t merely driven by brand idealism—it is accelerated by impending legal enforcement and changing consumer habits worldwide.
| Rejyon / Règleman | Key Requirement | Impact on Packaging Design |
| EU PPWR (Anbalaj & Packaging Waste Regulation) | All packaging placed on the EU market must be fully recyclable by 2030, with strict performance grades. | Outlaws unseparable multi-material composites; mandates high-purity mono-streams. |
| EPR (Pwolonje Responsablite Pwodiktè) Tariffs | Brand owners pay fees based on the recyclability and weight of their packaging materials. | Multi-layer packaging faces severe financial penalties; mono-materials earn lower eco-fees. |
| UK Plastic Packaging Tax | Applies to plastic packaging with less than 30% kontni resikle. | Mono-material PE/PP structures make incorporating high-grade PCR (Post-Konsomatè resikle) content technically feasible. |
Beyond legal mandates, major global brands have publicly committed to 100% ki kapab itilize ankò, resikle, or compostable packaging goals. Companies that fail to redesign their portfolio risk facing retail penalties, consumer backlash, and higher operational fees.
Overcoming Real-World Manufacturing Challenges
Transitioning your product portfolio to a mono-material format requires careful planning. Packaging teams often encounter three core operational friction points:
- Narrow Thermal Windows on Converting Lines:Because the entire structure belongs to the same resin family, the melting point difference between the print layer and the seal layer is significantly narrower than in PET/PE constructions.
- Fix: Upgrade to precise impulse sealing equipment or integrate ultrasonic sealing technologies to isolate heat application.
- Haze and Optical Clarity Drops:Unoriented PE naturally exhibits higher haze than optical-grade PET.
- Fix: Utilize MDO-PE films combined with reverse-printed high-gloss varnish systems to maintain premium visual shelf appeal.
- Flex-Cracking in High-Barrier Layers:Ultra-thin barrier coatings ($\tèks{SiO}_x$/$\text{AlO}_x$) can develop micro-fractures during transport or aggressive pouch forming.
- Fix: Formulate hybrid barrier lacquers or utilize nano-composite coatings that flex without compromising OTR/WVTR performance.
Actionable Checklist for Brand Owners
If you are evaluating mono-material flexible packaging for an upcoming product launch or redesign, keep these four implementation steps in mind:
- Map Your Barrier Needs Precisely: Don’t over-engineer. Measure the exact OTR and WVTR threshold your product requires for its intended shelf life rather than defaulting to maximum foil-level protection.
- Engage Equipment Vendors Early: Test mono-PE or mono-PP rollstock on your existing Form-Fill-Seal (FFS) ekipman. Gauge thermal response and web tension limits before committing to large supplier orders.
- Verify Recyclability Certification: Work with third-party testing bodies (such as RecyClass or APR) to ensure your final package—including inks, adhésifs, valves, and zippers—passes localized circular economy criteria.
- Design for the Complete Package: Remember that fitments, spouts, and recloseable zippers must share the same resin family. A mono-PE pouch with a polypropylene zipper negates the mono-material advantage and risks stream rejection.
The Path Ahead
The future of flexible sustainable packaging lies in simplicity. By stripping away incompatible composite layers and embracing single-polymer engineering, brands can build high-performing, commercially viable packaging structures that seamlessly integrate into existing mechanical recycling infrastructure. Moving to recyclable mono-material solutions isn’t just about meeting compliance deadlines—it’s about ensuring your product thrives in a circular economy.